If you’ve ever held a precision-engineered aerospace turbine blade, a medical implant part that fits exactly to a patient’s anatomy, or a complex automotive component that withstands extreme heat and pressure, chances are it was made via investment casting—one of the most reliable, versatile manufacturing processes for high-precision metal parts. As a third-generation investment casting supplier, I’ve walked every step of this process thousands of times, working directly with engineers, designers, and procurement teams to turn 2D designs into parts that hold up in the most demanding industries. Investment casting, sometimes called “lost wax casting,” isn’t just pouring metal into a mold; it’s a precise, multi-step sequence that balances artistry and engineering, where even a small misstep can ruin a critical part. Over the past 15 years in this space, I’ve seen clients underestimate how much goes into each step, so let’s break down exactly what goes into investment casting, straight from the floor of our shop. Investment Casting
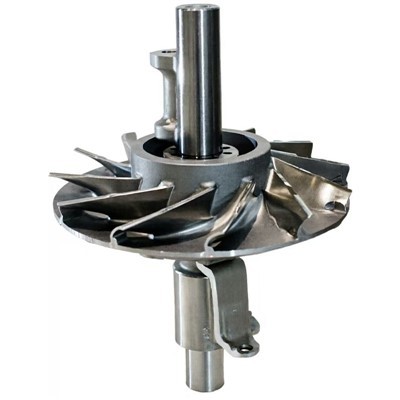
The entire process starts long before any metal touches a mold—it begins with translating your design into a functional, casting-ready blueprint. Many clients come to us with a 3D CAD file of a part they need, whether it’s a small medical bone plate or a large industrial pump housing. Our first step is always design validation, and this is where we add huge value that most general casting suppliers skip. We know that metal shrinks as it cools, that certain wall thicknesses will cause porosity, and that draft angles (the slight tapers needed to remove a part from the mold) can make or break your final part’s fit. For example, a client once brought us a tiny dental implant with a uniform 0.8mm wall thickness; our design team flagged that this would trap air during casting, leading to voids that would make the implant unsafe for surgical use. We adjusted the wall to 1mm in critical areas and added tiny gating points (the channels that feed molten metal into the mold) to vent air, cutting down on scrapped parts by 40% for that order. We also work with clients to select the right alloy for their use case: stainless steel, aluminum, titanium, or superalloys for aerospace. Once the design is signed off, we move to creating the master pattern—the single, exact version of your part that will be used to make the rubber molds for mass production.
Making the master pattern is where precision becomes non-negotiable. For low-volume orders, we machine a solid metal master from a block of the alloy you’ll use, but for high-volume runs, we use a 3D printed master, usually made from photopolymer resin that matches the shrink rate of your chosen metal. Our in-house 3D printing lab uses industrial resin printers that have a tolerance of ±0.05mm—less than the width of a human hair—so the final part matches your CAD file perfectly. We then use this master to create a rubber mold, injecting liquid silicone around the master and letting it cure for 12 hours. Once cured, we split the rubber mold, remove the master, and are left with a cavity that duplicates your part. Next, we inject molten wax into this rubber mold under low pressure (around 10 PSI) to create individual wax patterns. We do this in temperature-controlled rooms, because wax expands and contracts with even small shifts in temperature; a room that’s 72°F vs. 75°F can change a pattern’s size by 0.1mm, which throws off the entire part. Each wax pattern is inspected with a coordinate measuring machine (CMM) before moving on, because even a slightly warped wax pattern will result in a bad metal part.
Once we have individual wax patterns, we attach them to a wax sprue, a central wax rod that acts as a channel for molten metal to flow into the part. We also attach wax runners and gates to connect each part to the sprue, and add a ceramic cup at the bottom of the sprue to catch any excess metal (this is called a “feed cup,” and it ensures that molten metal stays in the mold cavity until all air is pushed out, preventing porosity). For complex orders with multiple parts, we might attach 20 to 50 wax patterns to a single sprue, creating what we call a “tree.” Each tree is designed to balance weight and flow, so that when we pour metal, every part gets an even amount of material. We’ve had clients ask why we don’t just use a simpler tree design, but a poor tree layout can lead to parts with cold shuts (where two streams of metal don’t fully fuse) or incomplete fills. For example, an automotive client once brought us a tree that had parts arranged too closely together, leading to wax patterns breaking during the next step. We redesigned the tree to space parts 15mm apart and added support structures, cutting pattern breakage by 90% for that run.
The next, most time-consuming step is investing—building the ceramic mold that will hold the wax patterns. This is where the process gets its name “investment casting,” because the wax tree is fully invested (encased) in a ceramic slurry. First, we dip the entire wax tree into a fine, liquid ceramic slurry made of silica and binders. This first coat is critical: it’s the one that touches the wax pattern, so we use the finest ceramic grains to capture every detail of the part, down to small threads or surface textures. We then sprinkle a layer of very fine sand onto the wet slurry to reinforce it, and let it dry for 20 to 30 minutes. We repeat this process, building up coats of ceramic until the mold is 6 to 10mm thick—thick enough to withstand the pressure of molten metal inside. For large industrial parts, we might add up to 8 coats, while small medical parts only need 4. This step takes 1 to 2 days per tree, and every coat is inspected for cracks or uneven coverage; even a tiny crack can let molten metal leak out during pouring, ruining the entire tree.
Once the ceramic mold is fully dried and cured, we need to remove the wax inside—this is the “lost wax” part of the process. We load the ceramic mold into an autoclave, a large pressure vessel that uses steam at 150°C and 80 PSI to melt and flush out all the wax. The wax is recovered and reused, which cuts down on waste for our clients. Once all the wax is gone, we’re left with a hollow ceramic mold cavity that exactly matches your part. We then bake the mold in a kiln at 1,000°C for 12 hours, a step called burnout. Baking removes any remaining moisture or binders from the ceramic, and preheats the mold so that when we pour molten metal, the mold doesn’t crack from thermal shock. This preheating step is another common area where suppliers cut corners—skipping a full burnout can lead to mold failure during pouring, and it’s a mistake I see too often when clients get quotes from overseas suppliers that skip this to save time. Our kilns are monitored 24/7 during burnout, so we know exactly when the mold is ready for metal.
Now comes the moment of truth: pouring the molten metal. We melt metal in an induction furnace, which heats the alloy to 1,500 to 1,800°C, depending on the metal type—enough to make titanium flow like water, or stainless steel molten and fluid. Once the metal is at the correct temperature, we take the preheated ceramic mold out of the kiln and immediately pour the metal into the feed cup at the top of the sprue. The hot mold keeps the metal molten as it flows down the sprue, through the runners, and into each part cavity, filling every detail even the smallest features. We work in a clean room during this step, because even a speck of dust can cause a defect in the metal. For high-performance parts, we use vacuum pouring to eliminate air bubbles entirely, which is critical for aerospace and medical parts that can’t have internal porosity. After pouring, the metal cools and solidifies in the mold for 2 to 4 hours, depending on the part size.
Once the metal is solid, we break away the ceramic mold—this step is called knockout. We use hydraulic hammers and vibratory tumblers to remove the ceramic from the parts, then blast them with media (usually fine steel shot) to remove any remaining ceramic residue. Now, we have a rough metal part that looks like your design, but it still has the sprue, runners, and feed cup attached—we call these “gating remnants.” The next step is cutting off these remnants, which we do with precision band saws or CNC mills, depending on the part size and material. For small, delicate parts like medical implants, we use laser cutting to avoid damaging the part itself. After cutting, every part is cleaned and inspected to make sure no gating material is left behind. This is where I often work with our quality team to check for dimensional accuracy, using CMMs to verify that the part matches your CAD file within ±0.02mm, and doing non-destructive testing (X-rays, ultrasonic testing) to look for internal voids or defects—critical for parts used in medical or aerospace applications.
The final steps are finishing and post-processing, which turn the rough cast metal into a ready-to-use part. This includes surface grinding to smooth any rough edges, heat treatment to improve the metal’s strength (for example, annealing stainless steel parts to make them more durable), and polishing for parts that need a smooth finish. For parts that need tight tolerances, we do CNC machining on critical features, like holes or mounting points, to get the exact fit you need. We also offer secondary processes like passivation for stainless steel, which protects against corrosion, and coating for medical parts to make them biocompatible. Each part goes through a final inspection before it ships, with a full quality report that confirms dimensions, material composition, and any testing results—something many small suppliers don’t provide, but that’s non-negotiable for our clients.
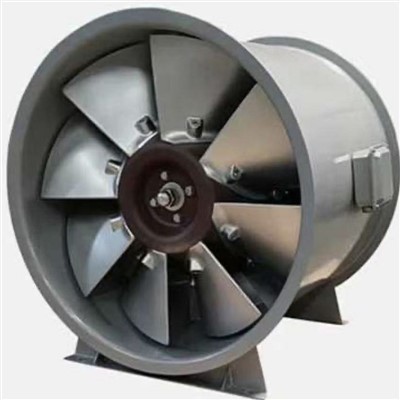
Every step in investment casting is designed to deliver precision parts that other manufacturing methods can’t match, especially for complex geometries. As a supplier, I’ve built our reputation on being transparent about each step—we want our clients to understand exactly what goes into their parts, so there are no surprises when they receive them. If you’re looking for a reliable investment casting partner, whether you need low-volume prototype parts or high-volume production runs tailored to your industry, reach out to our team to discuss your project. We work with clients across aerospace, medical, automotive, and industrial sectors, and we’re ready to turn your design into a part that meets your exact specifications.
Fan Impeller References
- Campbell, J. (2015). Castings Practice: The Ten Rules of Castings. Elsevier.
- ASM International. (2008). Investment Casting Handbook. ASM International.
- Brady, G. S., & Clauser, H. R. (2002). Materials Handbook: Materials, Properties, and Uses. McGraw-Hill.
- Investment Casting Institute. (2021). Standard Practices for Investment Casting. Investment Casting Institute.
Shandong Shunye Stainless Steel Co., Ltd.
Address: Shandong Province, Binzhou City, Wudi County, Liubao Town, Zhangdong Road, Duliucun Village
E-mail: sales@wdshunye.com
WebSite: https://www.shunyecasting.com/
